Choosing the right Barbed Wire Making Machine can shape production quality, operating costs, and customer trust. Global buyers must look beyond advertised speed. Wire diameter, barb spacing, coil size, and material compatibility affect daily performance. A machine may appear powerful, yet struggle with uneven galvanized wire or unstable feeding.
“Consistent output matters more than impressive speed,” says Daniel Mercer, an independent wire-processing equipment consultant. His point is practical. A reliable machine should form sharp, evenly spaced barbs while maintaining steady tension. Operators should also inspect the straightening unit, cutting system, take-up mechanism, and control panel before purchasing. Small weaknesses become expensive during long production runs.
This guide examines five machines for international buyers. It considers output capacity, automation, maintenance access, energy use, and technical support. Safety features matter too, including guarded moving parts, emergency stops, and clear operating instructions. Buyers should confirm applicable standards in their destination markets. They should also request sample production, factory references, warranty terms, and spare-parts availability.
Details matter.
A compact workshop may value simple controls and quick adjustments. A large manufacturer may need automatic lubrication, higher throughput, and data monitoring. However, the fastest model is not always the best choice. That assumption deserves reconsideration. Actual results depend on operator training, wire quality, installation conditions, and preventive maintenance.
Some supplier claims can sound attractive but remain difficult to verify. Careful buyers should compare documented specifications with real production samples. This approach reduces surprises and supports a safer, more dependable investment in modern fencing manufacturing.
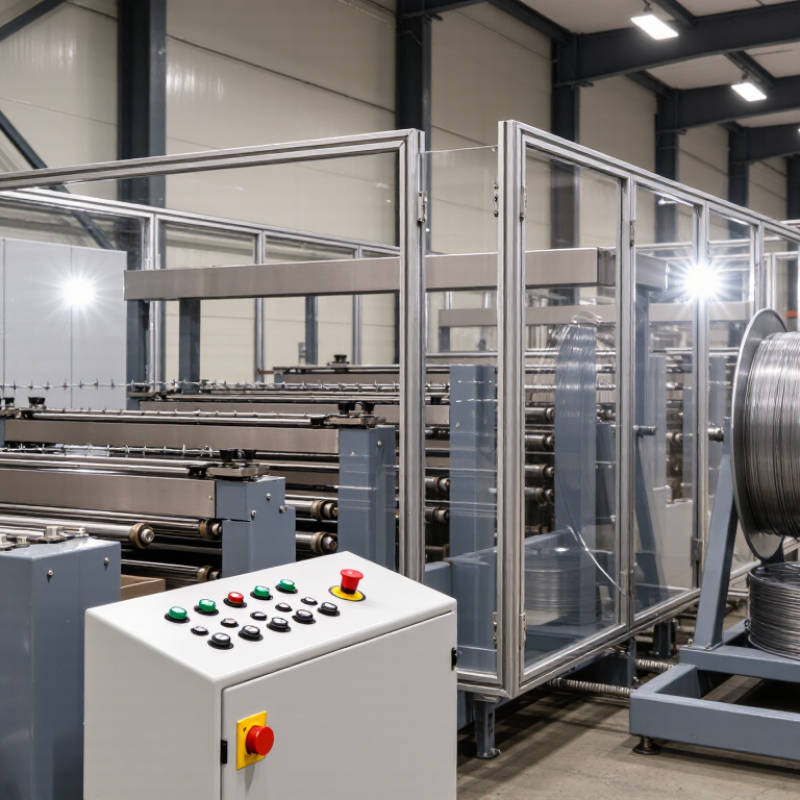
For global buyers, the best barbed wire machine is not always the fastest model. It must consistently produce 2.0–2.5 mm wire and support ASTM A121 requirements.
ASTM A121-22 covers zinc-coated steel barbed wire, including dimensions, tensile performance, barb spacing, and zinc-coating tests. It does not certify any machine itself.
Five practical choices include a double-twist machine, a single-twist machine, an automatic line, a high-tensile configuration, and a compact workshop model.
For 2.0–2.5 mm wire, check motor torque, straightening accuracy, die hardness, and tension control. A line that fluctuates by only a small amount can create uneven barbs. That detail matters during inspection.
The World Steel Association reported about 1.89 billion tonnes of crude steel production in 2023, showing the scale of available steel feedstock. However, feedstock volume does not guarantee stable wire quality.
Tips:
Request a sample run before purchase. Measure wire diameter at several points. Test zinc adhesion after twisting. Ask for calibration records and ASTM A121 test references. Do not trust speed figures alone.
I once considered output rate the main buying factor. That was too narrow. In practice, maintenance access and wire break recovery often decide real productivity.
Also review coating mass requirements carefully, because ASTM A121 includes different coating classes. Your target may need adjustment after local climate, transport, and installation trials. Never assume 2.0–2.5 mm automatically meets every project specification.
Double-twist lines suit buyers needing steady output and consistent strand formation. Their stated capacity reaches 40–100 kg/h, depending on wire diameter, coating, pitch, and operator settings. An eight-hour shift could produce 320–800 kg before stoppages. Real output is usually lower. Wire loading, spool changes, and adjustments consume time.
A 2024 Grand View Research report valued the global fencing market at approximately USD 30 billion in 2023. It also forecast continued growth through 2030. This supports demand for efficient fencing-wire production, especially in agricultural and infrastructure projects. During machine trials, inspect twist tightness, barb spacing, wire tension, and finished coil weight. A practical test should run several hours, not only a short demonstration.
Maintenance matters. Check gearbox noise, cutter wear, lubrication access, and electrical safety features. The 40–100 kg/h range sounds attractive, but it is not a guarantee. Thicker wire can reduce speed sharply. Galvanized wire may also require careful tension control. I would compare actual trial results with the supplier’s specification sheet and local technical standards before ordering. One overlooked detail can become an expensive production habit.
Galvanizing systems designed for 50–300 g/m² zinc coating give barbed wire producers useful control over corrosion protection. The lower range suits moderate environments and cost-sensitive orders. Heavier coatings support longer outdoor service in humid or industrial areas. Buyers should examine coating stability, not only the maximum output.
During machine evaluations, check the zinc bath temperature, wire speed, wiping system, and take-up tension. These settings directly affect coating weight and surface smoothness. A reliable line should maintain even coverage across different wire diameters. It should also allow quick adjustment between production batches. Small variations can create bare spots or excess zinc.
Measurement matters. Use regular weighing tests and calibrated coating gauges. Record results beside line speed and bath conditions. This creates traceable production evidence for quality reviews. Operators also need safe access to heating zones, cleaning points, and moving components. Poor access often increases maintenance delays. I once underestimated the value of simple inspection windows; that was a costly oversight. The machine performed well, but troubleshooting became slower than expected. Buyers should request sample runs before purchase. Examine adhesion, coating uniformity, wire flexibility, and zinc consumption. Energy use and replacement-part availability deserve equal attention. A system may achieve 300 g/m², yet waste material at lower settings. That weakness can affect long-term operating costs.
PVC-coating lines cover a useful wire range, from thin 0.4 mm strands to heavier 4.0 mm cores. This flexibility suits fencing, agricultural, and general construction applications. MarketsandMarkets’ Wire and Cable Market report projects growth from about USD 202.3 billion in 2023 to USD 276.7 billion by 2028. That expansion increases demand for stable insulation and corrosion-resistant surfaces.
A practical line needs controlled pay-off, preheating, extrusion, cooling, diameter measurement, and take-up. For thin wire, tension control is critical because small fluctuations can create uneven coating or breaks. For 4.0 mm wire, the extruder needs stronger torque and steady material feeding. PVC processing temperatures often sit near 160–200°C, but the compound supplier’s data must guide final settings. Guesswork is expensive.
PlasticsEurope reported global plastics production of 400.3 million tonnes in 2022. PVC remains important, although production volume alone does not guarantee coating quality. Buyers should inspect melt-pressure stability, cooling length, gauge accuracy, and changeover time. I would not trust a brochure’s maximum speed without testing the actual wire diameter.
A factory trial should measure coating thickness at several points, especially after start-up and reel changes. The overlooked detail is operator training; even a precise line can produce inconsistent output when temperature or tension adjustments are made too quickly.
Best Machine Four is an automatic barbed wire line designed for consistent 45–75 mm barb spacing. This range suits many fencing projects, including farm boundaries and perimeter barriers. The line usually combines wire straightening, twisting, barb forming, and take-up functions. Automation reduces repeated manual adjustments and keeps production moving steadily. However, actual output depends on wire diameter, material strength, and operator settings.
In practical use, stable tension is critical. If the feed wire slips, barb spacing may drift by several millimeters. A reliable machine should provide adjustable feeding rollers, clear spacing controls, and emergency shutoff access. Before purchasing, ask for trial production using your intended wire grade. Check the finished coil for sharp barb formation, even twisting, and smooth winding. I would not judge a line by speed alone. A faster machine can create more waste when calibration is poor.
Tips: Measure spacing at several points, not just one section. Keep rollers clean and inspect cutting tools regularly. Record settings for each wire specification. This simple log can save hours during repeat production. Also, leave room for improvement. Even a well-built automatic line may need occasional spacing corrections after extended operation. Train operators to notice unusual vibration, loose coils, or uneven barbs before these problems affect a full batch.
Typical technical data for fully automatic double-twist barbed wire production lines
| Specification | Typical Data | Practical Relevance for Global Buyers |
|---|---|---|
| Machine configuration | Fully automatic double-twist barbed wire line | Automatically feeds, twists, forms barbs, cuts, and winds the finished coil with limited operator intervention. |
| Adjustable barb spacing | 45 mm, 60 mm, and 75 mm; other settings may be available within the machine’s adjustment range | Supports common fencing requirements for farms, boundary protection, security fencing, and infrastructure projects. |
| Main line-wire diameter | Approximately 2.0–3.5 mm | Covers widely used low-carbon steel line-wire sizes; the actual range depends on tooling and motor configuration. |
| Barb-wire diameter | Approximately 1.8–2.5 mm | Suitable for standard commercial barbed wire when matched with compatible line-wire dimensions. |
| Wire material | Low-carbon steel wire; galvanized, zinc-coated, or PVC-coated wire can be used when compatible with the feeding and twisting system | Material selection affects corrosion resistance, finished-wire appearance, tool wear, and operating cost. |
| Production speed | Approximately 35–70 m/min, depending on wire diameter, barb spacing, and coil specifications | Actual output should be confirmed using the buyer’s selected wire size and required barb pattern. |
| Typical output capacity | Approximately 40–90 kg/h | Production weight varies because heavier wire and shorter barb spacing consume more material per finished metre. |
| Finished coil diameter | Commonly 300–500 mm, adjustable according to the winding unit | Compact coils are easier to handle and transport, while larger coils can reduce packing frequency. |
| Common coil length | Typically 100–500 m per coil | The final coil length should be selected according to local sales units, packaging limits, and handling equipment. |
| Installed electrical power | Approximately 7.5–15 kW for the main machine and auxiliary units | Electrical load depends on the number of pay-off units, winding system, control cabinet, and selected automation level. |
| Power supply options | Common industrial supplies include 380–415 V, three-phase, 50 Hz; other voltages may require configuration changes | The buyer should confirm local voltage, frequency, phase arrangement, grounding, and electrical-safety requirements before ordering. |
| Typical line footprint | Approximately 8–14 m long × 3–5 m wide, excluding material storage and operator access areas | Adequate space is needed for wire pay-off, finished-coil removal, maintenance, and safe material movement. |
| Control system | Digital control panel with variable-speed adjustment, emergency stop, and fault indication | Simplifies setting changes between 45 mm, 60 mm, and 75 mm barb spacing and helps reduce operator error. |
| Automation functions | Automatic wire feeding, barb forming, twisting, length counting, cutting, and coil winding | Reduces manual handling and helps maintain consistent barb spacing and finished-coil length. |
| Recommended staffing | Usually 1 operator per line during normal production, with additional support for loading and packing | Labour requirements vary with coil weight, raw-wire handling, packaging method, and plant layout. |
| Safety provisions | Protective guards, emergency-stop circuits, enclosed transmission parts, and wire-break or overload protection | Safety functions should be checked against the installation country’s workplace and machine-safety regulations. |
| Best-fit applications | Agricultural fencing, livestock enclosures, property boundaries, perimeter security, and infrastructure protection | The 45–75 mm spacing range provides flexibility for both general-purpose and higher-density fencing products. |
| Buyer verification checklist | Request a production test using the intended wire grade, diameter, coating, barb spacing, coil length, and local power supply | A sample test is the most reliable way to confirm speed, wire consumption, spacing accuracy, coil quality, and actual energy demand. |
Choosing the right Barbed Wire Making Machine is essential for global buyers seeking consistent quality, efficient production, and reliable operation. The best systems should support common standards such as ASTM A121 and handle wire sizes around 2.0–2.5 mm. Double-twist production lines can deliver approximately 40–100 kg per hour, while galvanizing systems provide durable zinc coatings of about 50–300 g/m² for improved corrosion resistance.
For specialized applications, PVC-coating lines may process wire from 0.4–4.0 mm, offering additional protection and color options. Fully automatic machines with adjustable barb spacing between 45 and 75 mm can improve productivity and product consistency. Buyers should also compare energy consumption, operator safety, maintenance requirements, automation levels, and quality-control performance. By evaluating these technical factors together, companies can select a practical barbed wire production solution that supports stable output, long service life, and compliance with applicable market standards.
Get in Touch
570 Alden Road Unit #10, Markham Ontario Canada, L3R 8N5
Quick Links
Featured Products
Industries